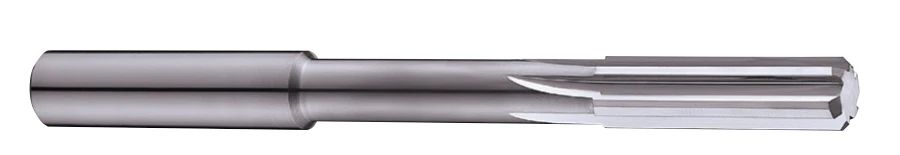
Straight Flute Carbide Reamers
For blind and through holes. A versatile starting point when both hole types appear on the same purchasing list. Confirm stock allowance and chip clearance for each application.
View Dimensions & ApplicationsPDF page 1KY TOOLS / Reamers
For blind and through holes. A versatile starting point when both hole types appear on the same purchasing list. Confirm stock allowance and chip clearance for each application.
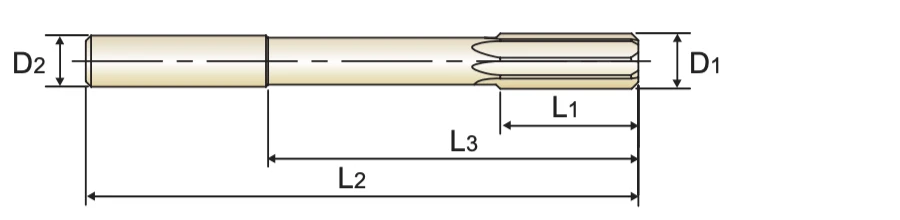
For blind and through holes. A versatile starting point when both hole types appear on the same purchasing list. Confirm stock allowance and chip clearance for each application.
View Dimensions & ApplicationsPDF page 1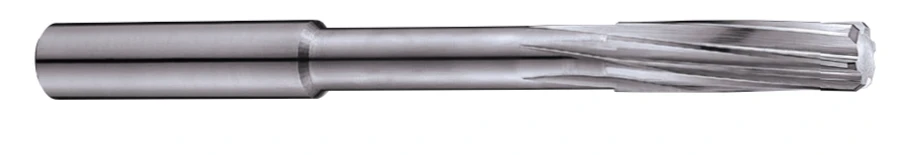
Recommended for blind holes; also suitable for through holes. The right-hand spiral helps return chips towards the entry, where bottom clearance and coolant access need careful review.
View Dimensions & ApplicationsPDF page 2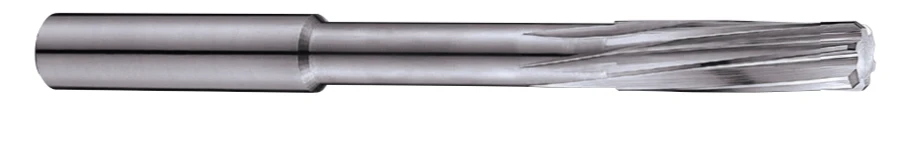
For through holes. The left-hand spiral directs chips towards the exit. Keep exit clearance available; left-hand spiral describes the flute helix, while cutting remains right-hand.
View Dimensions & ApplicationsPDF page 3DIN 1420 reamer diameter tolerance for H7 holes
Target hole finish: Ra ≤ 1.6 μm
Unequal flute spacing
Cylindrical shank: DIN 6535-HA
Confirm the finished-hole limits, surface finish and inspection method with your RFQ. H7 and Ra are application targets; results depend on material, pre-hole quality, stock allowance, runout and coolant.
Ø2–20 mm / 28
L3 is the shoulder-to-tip length shown in the drawing. L2 is overall length. All dimensions are in mm.
| Cutting diameterD1 | Shank diameterD2 | Flute lengthL1 | Shoulder-to-tip lengthL3 | Overall lengthL2 | FlutesZ | Request a Quote |
|---|---|---|---|---|---|---|
| 2.0 | 4 | 11 | 20 | 50 | 4 | Request a Quote |
| 2.5 | 4 | 14 | 26 | 57 | 4 | Request a Quote |
| 3.0 | 4 | 15 | 31 | 61 | 6 | Request a Quote |
| 3.5 | 4 | 18 | 36 | 70 | 6 | Request a Quote |
| 4.0 | 4 | 19 | 42 | 75 | 6 | Request a Quote |
| 4.5 | 6 | 21 | 46 | 80 | 6 | Request a Quote |
| 5.0 | 6 | 23 | 51 | 86 | 6 | Request a Quote |
| 5.5 | 6 | 26 | 56 | 93 | 6 | Request a Quote |
| 6.0 | 6 | 26 | 56 | 93 | 6 | Request a Quote |
| 6.5 | 8 | 28 | 62 | 101 | 6 | Request a Quote |
| 7.0 | 8 | 31 | 68 | 109 | 6 | Request a Quote |
| 7.5 | 8 | 31 | 68 | 109 | 6 | Request a Quote |
| 8.0 | 8 | 33 | 74 | 117 | 6 | Request a Quote |
| 8.5 | 10 | 33 | 74 | 117 | 6 | Request a Quote |
| 9.0 | 10 | 36 | 80 | 125 | 6 | Request a Quote |
| 9.5 | 10 | 36 | 80 | 125 | 6 | Request a Quote |
| 10.0 | 10 | 38 | 86 | 133 | 6 | Request a Quote |
| 10.5 | 12 | 38 | 86 | 133 | 6 | Request a Quote |
| 11.0 | 12 | 41 | 95 | 142 | 6 | Request a Quote |
| 12.0 | 12 | 44 | 104 | 151 | 6 | Request a Quote |
| 13.0 | 16 | 44 | 104 | 151 | 6 | Request a Quote |
| 14.0 | 16 | 47 | 108 | 160 | 8 | Request a Quote |
| 15.0 | 16 | 50 | 110 | 162 | 8 | Request a Quote |
| 16.0 | 16 | 52 | 118 | 170 | 8 | Request a Quote |
| 17.0 | 20 | 54 | 121 | 175 | 8 | Request a Quote |
| 18.0 | 20 | 56 | 128 | 182 | 8 | Request a Quote |
| 19.0 | 20 | 58 | 129 | 189 | 8 | Request a Quote |
| 20.0 | 20 | 60 | 135 | 195 | 8 | Request a Quote |
No. All three listed geometries are right-hand cutting. Spiral direction describes the flute helix and chip flow, not the spindle rotation.
Reaming finishes an existing hole. Confirm pre-hole position, straightness and allowance before selecting the reamer; a precision diameter alone does not correct hole location.
Send the finished-hole drawing, limits, reach and work material. Request a drawing review for custom dimensions, coating or inspection requirements before ordering.
Send hole diameter and tolerance, blind/through hole and depth, workpiece material and hardness, pre-hole size, coolant arrangement, quantity and annual demand. For repeat orders or distribution, include coating, packaging and inspection-report requirements. Price, minimum order quantity and lead time are confirmed against your specification.
FROM OUR WORKSHOP
Two videos filmed in our workshop: CNC tool grinding and dimensional inspection.
See how we use a CNC grinder to make carbide end mills, drills and special cutters.
Watch on YouTubeWatch our ZOLLER inspection process for precision carbide end mills.
Watch on YouTube